
FlowTex GSC NW Nonwoven Sand Containers
Nonwoven geosynthetic sand containers for coastal revetments, dune protection, scour defence and shoreline rehabilitation across African coastlines. Seven grades from 40kg flood-response units to 4,000kg breakwater core bags, manufactured in our own Johannesburg facility from virgin-grade polypropylene continuous filament needle-punched nonwoven geotextile. Custom dimensions, fabric weights and seam configurations to order.
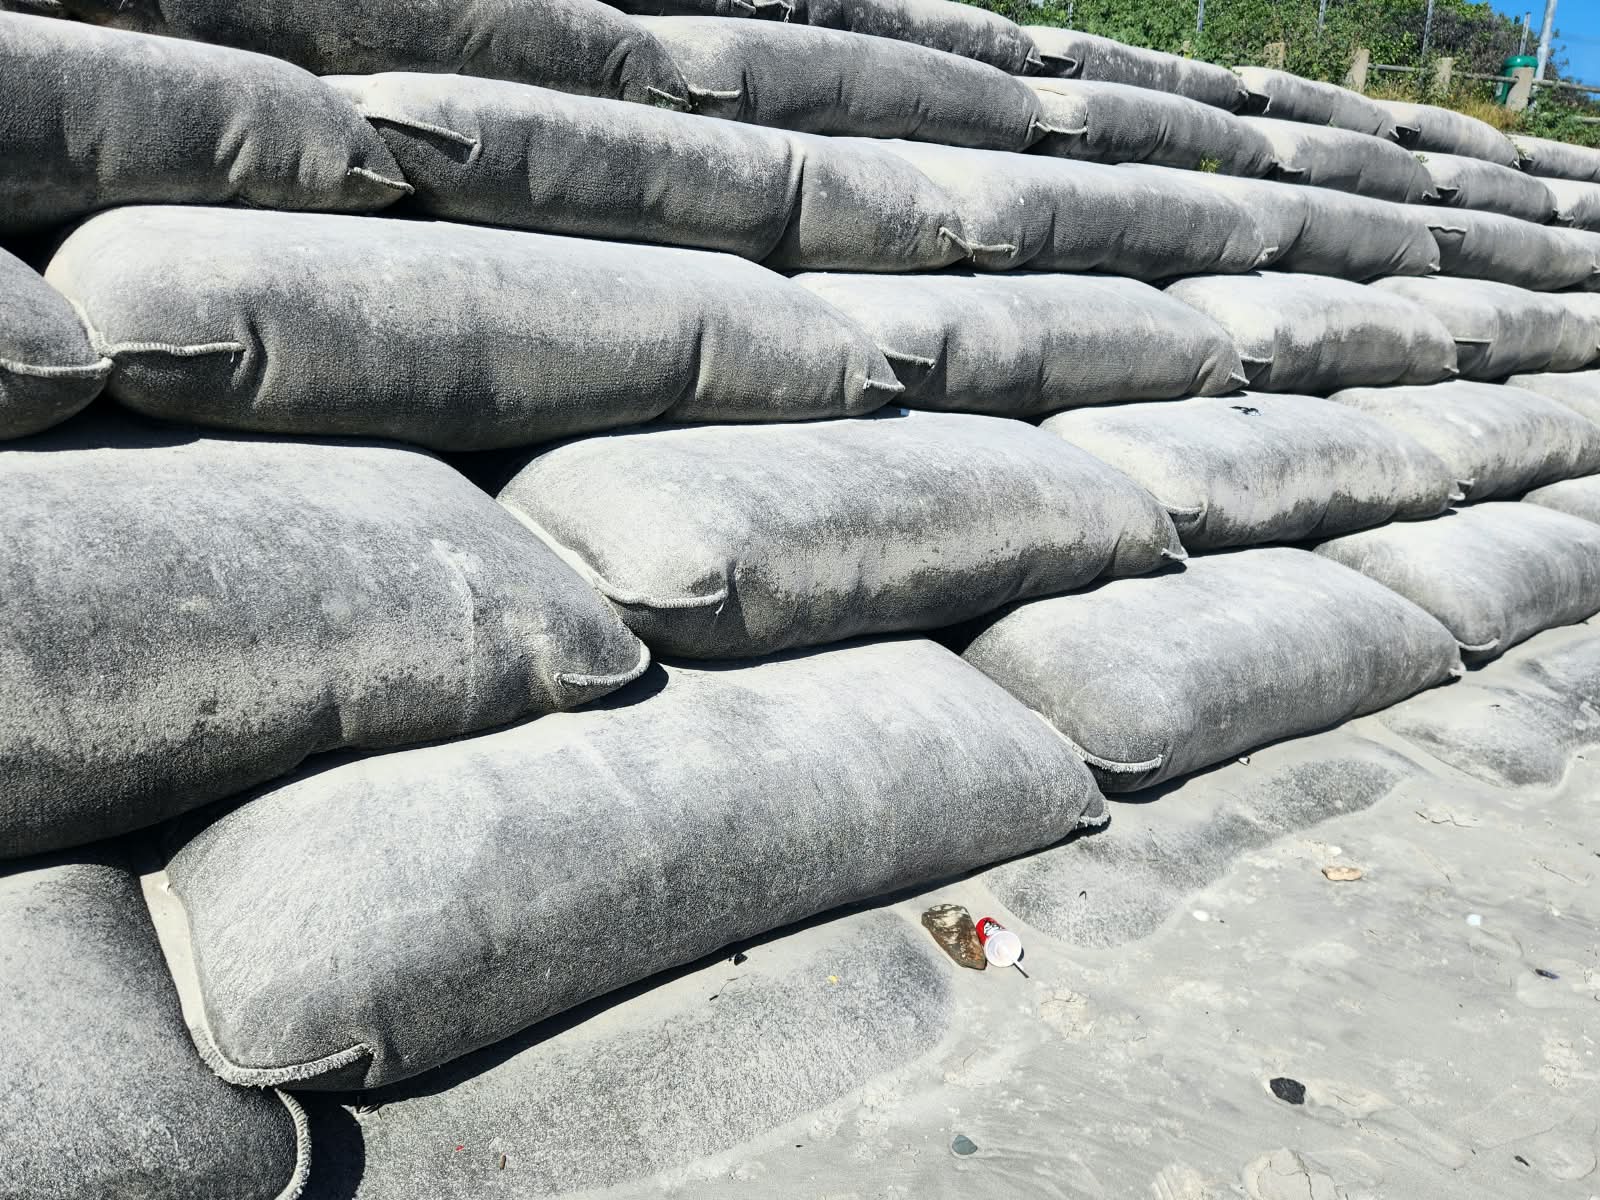
Technical Specification of FlowTex GSC NW Nonwoven Sand Containers
Nonwoven geosynthetic sand containers are engineered marine and hydraulic armour units, fabricated from needle-punched continuous filament polypropylene and filled on site with local sand to form monolithic, permeable, high-mass placed elements. They are specified for coastal revetments, dune-toe and cliff-toe protection, harbour scour defence, riverine bank reinforcement and shoreline rehabilitation. Seven grades, 40kg to 4,000kg.
Nonwoven is the correct construction wherever the container meets irregular or sharp substrate, rock armour or angular fill. Three properties govern. The entangled fibre structure spreads point loads across a diffuse contact area rather than into individual yarns, giving CBR puncture of 2.40 to 11.30 kN (EN ISO 12236). Elongation of 68 to 105 percent (EN ISO 10319) lets units deform and interlock as the structure settles. And opening size of 110 down to 70 micron (EN ISO 12956) retains fine coastal sand that a coarser woven fabric would pass.
Fabric is 100% virgin-grade polypropylene continuous filament - never recycled, regenerated or blended stock, which carries inconsistent molecular weight, uncontrolled additive migration and embrittled fibre segments. Published performance: chemical resistance above 90% (EN 14030), microbiological above 95% (EN 12225), weathering above 90% (EN 12224), UV strength retention 70 to 80% after 500 hours (ASTM D4355).
The range is cut, stitched and seam-tested in our own Johannesburg facility, so container geometry, fabric weight and closure specification are design variables rather than catalogue constraints - a non-standard footprint or a heavier cloth on a standard footprint is a production run, not an import lead time. All closures are double-seamed in UV-stabilised yarn, verified to EN ISO 10319. Single straight-seam closures are not supplied.
Every container ships with mill test certificates, independent third-party test data and full batch traceability against EN ISO 9864, 10319, 12236, 13433, 11058 and 12956, plus ASTM D4355. Manufacturing runs under ISO 9001:2015. Installation is executed under IAGI-aligned QA/QC with photographic sign-off at each course before the next is placed.
Typical Values for GEOSYNTHETIC SAND CONTAINERS
Properties & Dimensions
| Grade | Lay-Flat | Filled Mass | Fabric | Tensile | CBR Puncture | O90 | Application |
|---|---|---|---|---|---|---|---|
| NW40 | 0.60 × 0.40 m | 40 kg | 200 g/m² | 16 kN/m | 2.40 kN | 110 µm | Flood response |
| NW70 | 0.80 × 0.50 m | 70 kg | 200 g/m² | 16 kN/m | 2.40 kN | 110 µm | Flood response |
| NW70HD | 0.80 × 0.50 m | 70 kg | 300 g/m² | 21 kN/m | 3.60 kN | 90 µm | Riverine erosion |
| NW400 | 1.30 × 0.85 m | 400 kg | 800 g/m² | 55 kN/m | 9.20 kN | 80 µm | Low-energy coastal |
| NW1350 | 1.80 × 1.50 m | 1,350 kg | 800 g/m² | 55 kN/m | 9.20 kN | 80 µm | Medium-energy coastal |
| NW1800 | 2.36 × 1.45 m | 1,800 kg | 800 g/m² | 55 kN/m | 9.20 kN | 80 µm | High-energy coastal |
| NW4000 | 2.50 × 2.00 m | 4,000 kg | 1,200 g/m² | 80 kN/m | 11.30 kN | 70 µm | Extreme / breakwater |
Popular Catalogue Items
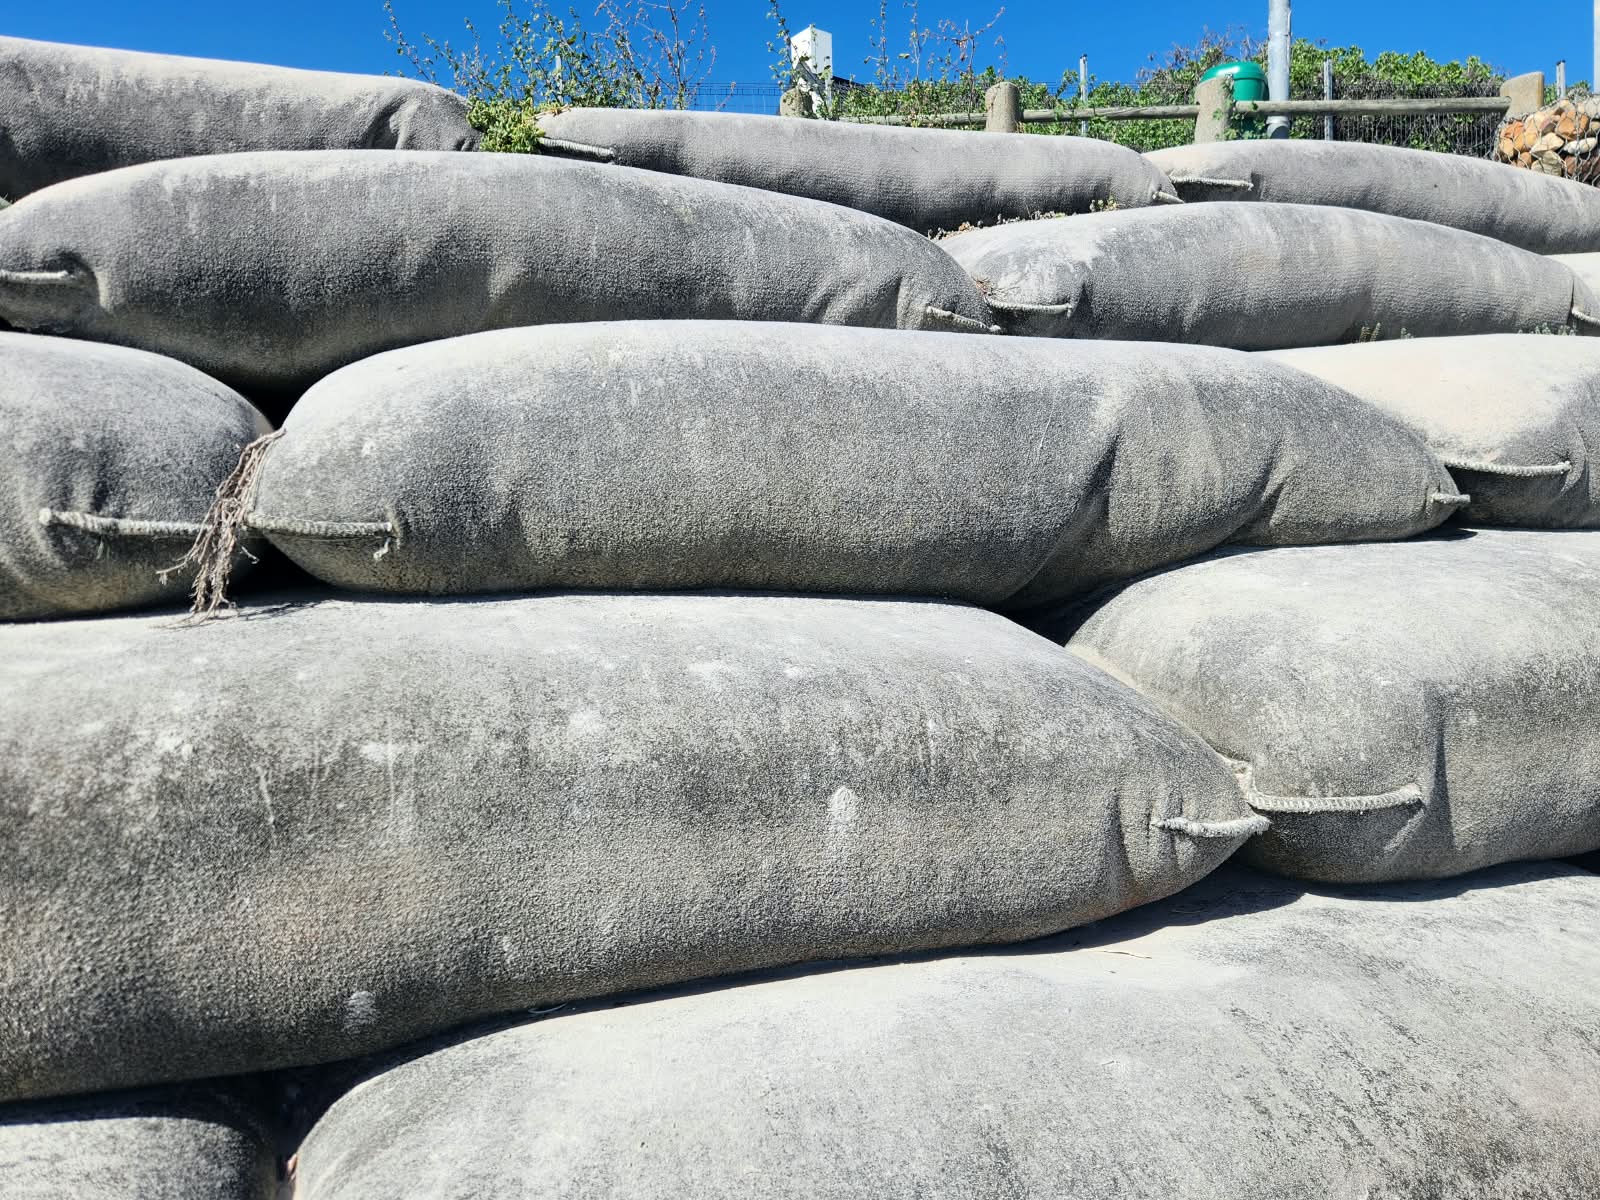
FlowTex™ GSC NW - Nonwoven Geosynthetic Sand Containers
40 kg to 4,000 kg , Tenara® UV-stable ePTFE threadRelated Product Groups
Three Questions To Ask Before You Order
1.How do I size a container against my design wave height?
2.What should the specification clause actually say?
3.Will the fabric retain my site sand?
4.What test data is supplied with delivery?
5.What is the design life, and what governs it?
6.When should I specify woven instead?
7.Can you manufacture a size or fabric weight that isn't in the range?
8.How deep does the toe need to be embedded?
Specification For The Design, Installation Of FlowTex GSC NW Nonwoven Sand Containers
Site preparation. - Excavate to firm base material over the full length of the revetment section. Remove rocks, stumps, root systems and protrusions and backfill the resulting cavities with sand compacted flush - irregular base surfaces prevent uniform bag contact and create stress concentrations under wave loading. Shape the slope to the design batter angle, toe elevation, crest elevation and rear taper before any container is placed; the profile cannot be reshaped afterwards without disturbing installed work. Establish setting-out pegs at toe and crest along the full length, with intermediate references at each end of the working
Underliner. - Lay a nonwoven filter geotextile over the prepared section, covering the full slope length and the base of the toe trench, before any container is placed. It separates the structure from native soil to prevent fines migration under pore-pressure cycling, and provides a consistent bearing surface for the first course. Lap panels down the slope in a shingle pattern, upper panel beneath lower so downslope flow passes over the joint. Minimum overlap 500mm on stable subgrades, 1,000mm on soft or variable ground. Where differential settlement is expected, sew or thermally bond the overlaps rather than free-lapping.
Toe embedment. - Placement begins at the toe and proceeds up the slope. Set the first container along the front line with its longer dimension parallel to the shoreline - this establishes the datum for every course above, and any misalignment introduced here propagates upward. Embed the toe container to a minimum of 1.8 times the significant wave height below design water level, per USACE Coastal Engineering Manual and CIRIA Rock Manual guidance. Toe scour removes lateral support and drives forward rotation and progressive collapse; inadequate embedment is the most commonly documented cause of geotextile revetment failure. Verify against project design wave height before placing any course above the toe.
Filling and closure. - Fill to approximately 80% of theoretical volumetric capacity. Overfilling prevents units conforming to each other and destroys interlock; underfilling produces excessive deformation and creates voids that concentrate hydraulic pressure at joints. Fill must be clean, well-graded sand free of sharp debris, organic contamination and material finer than the container O90. Fill bottom corners fully without creasing or folding before closing. NW40 through NW1350 are filled by hopper or mechanical equipment; NW1800 and NW4000 may be hydraulically filled in place. All closures are double-seamed - a straight pass followed by a zigzag or overlock second pass in UV-stabilised yarn. Single straight-seam closures are not compliant for structural coastal applications.
Stacking and compaction.- Lay successive courses in stretcher bond, each container offset half a bag length from the course below. Never stack in vertical columns: continuous vertical joints open progressively under repeated hydraulic loading, where staggered placement distributes wave-induced force across multiple units. After a minimum run of three containers, level and compact the course with the back of the excavator bucket or a plate compactor before the next is placed. Double-layer configurations provide approximately 17% greater stability than single-layer of the same grade under equivalent wave conditions. Check face alignment against setting-out pegs at every course to prevent progressive drift.
Crest, backfill and sign-off. - Crest containers take wave run-up and overtopping in addition to direct attack; place them last and with the greatest care. Bench the rear profile to receive each successive course, folding the underliner back over completed sections and overlapping at each bench to prevent flanking flow behind the structure. Complete the crest fill, taper off with specified compacted backfill to design elevation, and level the exposed face with sand. Photographic records are taken of each course before the next is placed under IAGI-aligned QA/QC, producing a verifiable installation record for the full structure depth.
Featured Projects Across Africa
Related Resources
Common GEOTEXTILE SAND BAGS Applications
Request a Quote for This Product Family
Upload your BOQ, drawings, or specifications and our technical team will provide a detailed proposal.
Have a project? Start with us.
Get expert engineering support, reliable material supply, and best-in-class installation.